Press forming & deep drawing
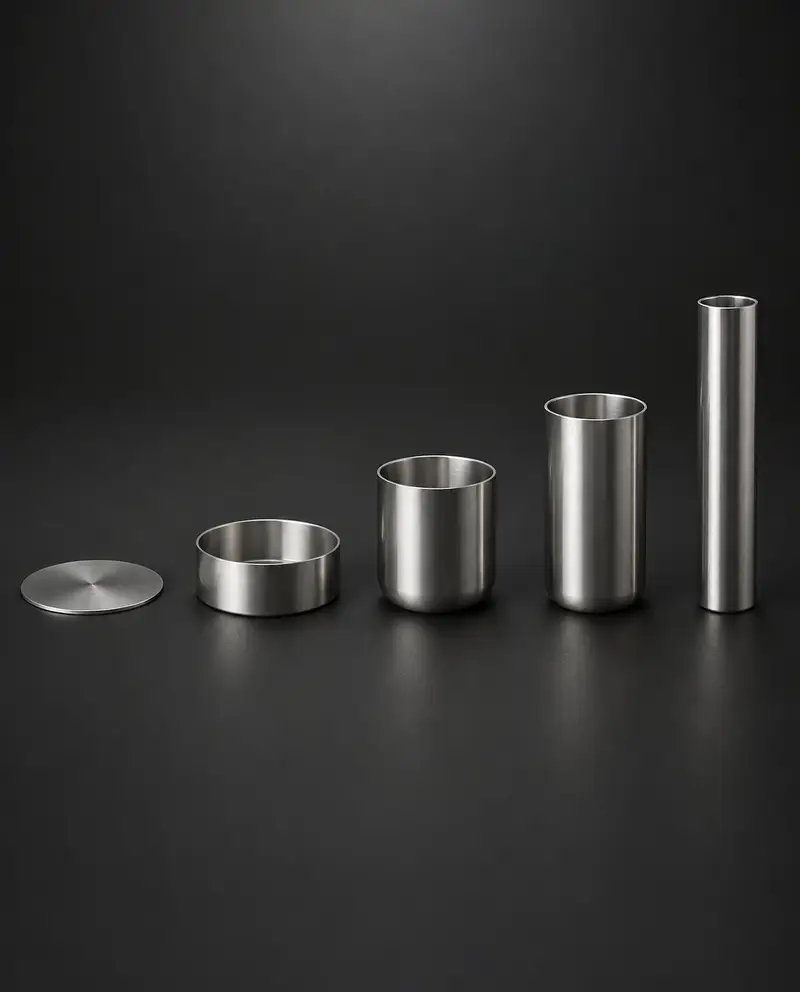
Hydraulic presses stretch flat metal into seamless, hollow shapes, which are then trimmed to length.
Press forming. CNC machining. Heat treatment. Finishing. We cut, press-form, heat-treat, pickle, machine, lap, mark and inspect metal parts in our two plants in Hyderabad.
Two plants · ISO 9001:2015 · AS9100-aligned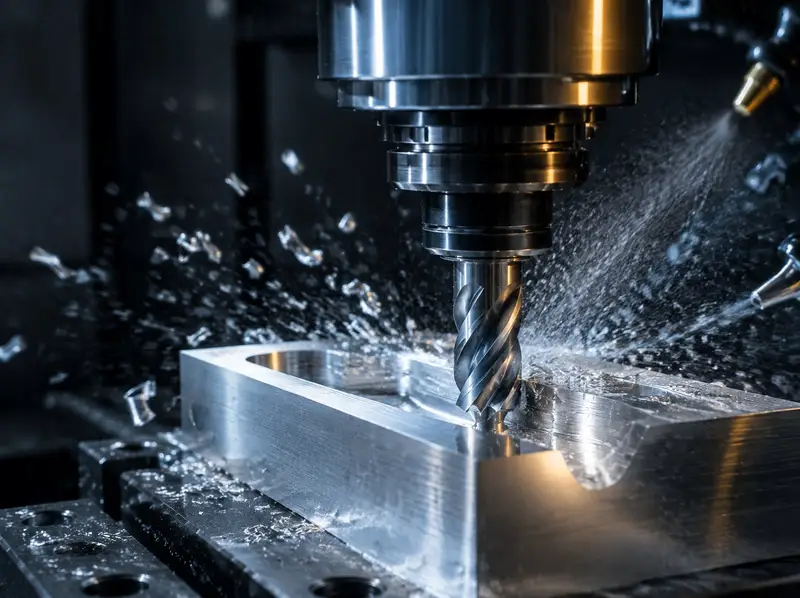
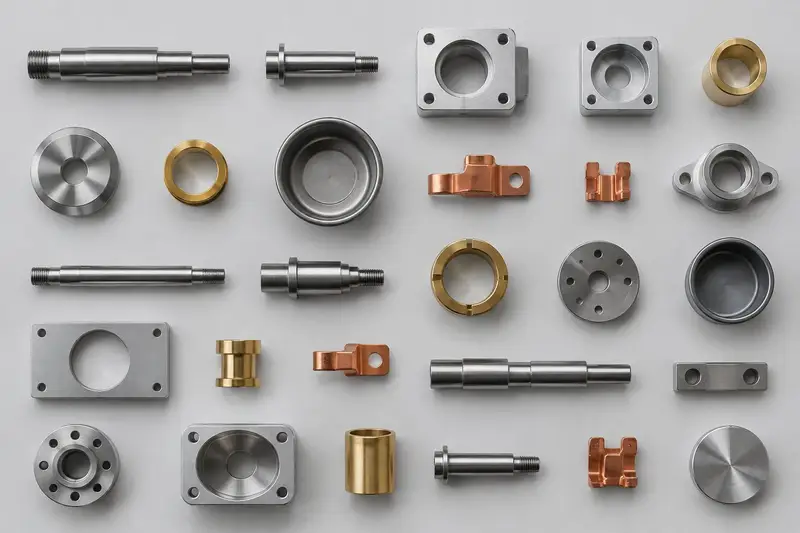
One order can cover every step, with one team responsible for the finished part. Six capabilities across two plants. Fewer suppliers, fewer handovers, one point of contact.
Hydraulic presses stretch flat metal into seamless, hollow shapes, which are then trimmed to length.
Computer-controlled turning and milling, including mill-turn and five-axis work, to ±0.0001″.
Annealing softens metal so it can be formed again. Induction hardening hardens just the zone that needs it.
An eight-tank pickling line dissolves the oxide layer (scale) that heat treatment leaves on metal.
Lapping for very flat, smooth surfaces. Laser marking for permanent part numbers. Spray painting.
Each feature measured against the drawing, with first-article inspection, SPC and lot traceability.
What each one does to the metal, and the machines we do it on. They are combined in whatever order your part needs.
| Process | What it does | Our equipment |
|---|---|---|
| 01 Cutting | A saw cuts bar and sheet stock to the length needed. | Band saw |
| 02 Press forming | A punch pushes flat metal into a die. The metal stretches into a seamless hollow shape. Nothing is cut away. | 2 × Mankoo and 1 × M.S.S.S. hydraulic presses · 10 T and 20 T presses |
| 03 Trimming | Forming leaves the open rim uneven. Trimming cuts the part to its final length. | Trimming machine |
| 04 Annealing | Forming makes metal harder and more brittle (work hardening). Heating then cooling it makes it soft and workable again. | Continuous annealing furnace · 50 kW induction annealing |
| 05 Induction hardening | An alternating magnetic field heats only the metal inside the coil. Rapid cooling (quenching) locks in hardness there. | 100 kW induction hardening · cooling tank |
| 06 Pickling | A chemical bath dissolves the oxide layer (scale) that heat leaves on metal, exposing clean metal. | 8 tanks · steam heating · overhead crane |
| 07 CNC machining | Computer-controlled cutting tools remove material to the exact dimensions on the drawing. | Ace Designers 540V · 2 × J300 LM · SJE 10 LM slant-bed lathe |
| 08 Lapping | A fine abrasive between the part and a flat plate wears down high spots, leaving a very flat, smooth surface. | Lapping machine |
| 09 Laser marking | A focused laser beam permanently marks numbers or codes into the surface. | Laser marking machine |
| 10 Inspection | Each feature is measured against the drawing. Hardness is tested against the specification. | Profile projector · hardness tester · micrometers · calipers · pitch gauges |
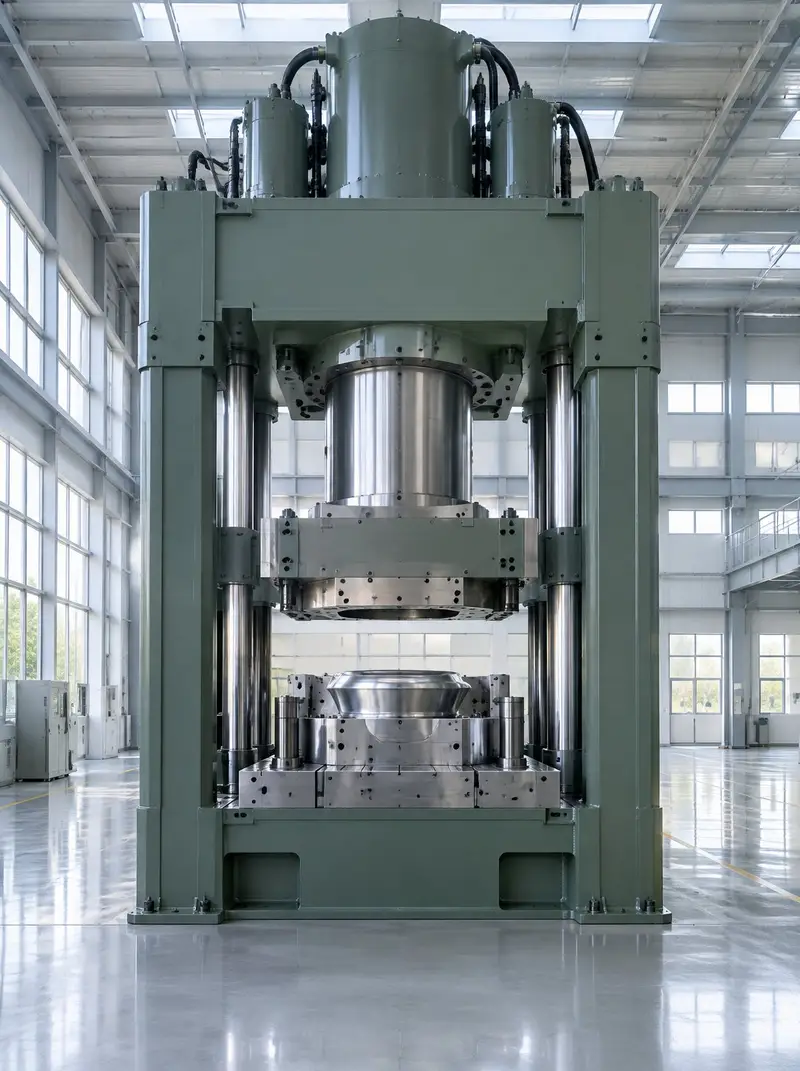
A punch pushes a flat metal disc into a die. The metal flows into a seamless cup. Repeat draws through smaller dies make the wall longer and thinner. Because nothing is joined, there is no weld or seam.
Blank › Cup › 1st draw › 2nd draw › 3rd draw › Trimmed
Machining more faces in one setup means the part is clamped fewer times, so small errors don't add up. Parts are measured while still on the machine.
Every size and tolerance on your drawing is a requirement. We machine to each one, then measure and report against it before production starts.
How far a size may vary. ±0.010 means up to 10 µm either way.
First-article inspection. The first parts are fully measured before production runs.
Statistical measures of how consistently a process holds tolerance, part after part.
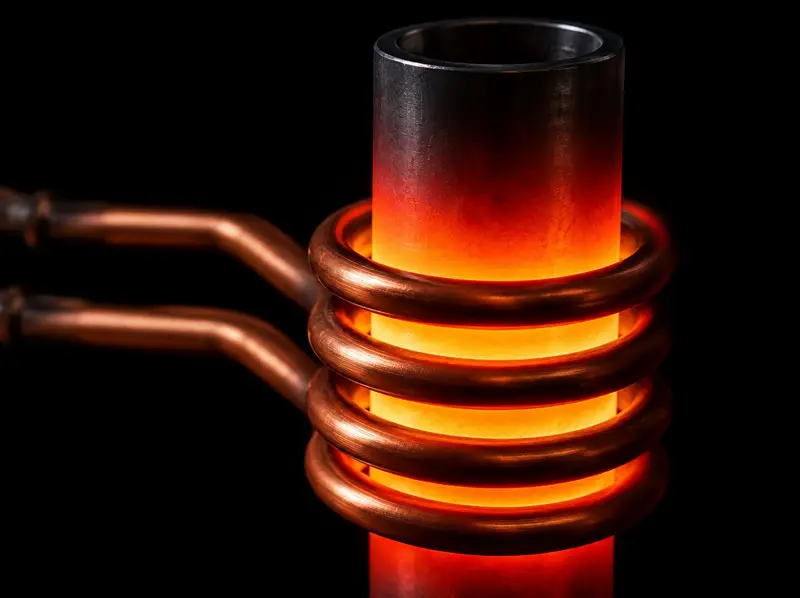
A continuous annealing furnace softens whole parts. 50 kW induction annealing softens a selected zone. 100 kW induction hardening, followed by rapid cooling. Heat number, machine cycle and operator recorded for each lot; verified on our in-house hardness tester.
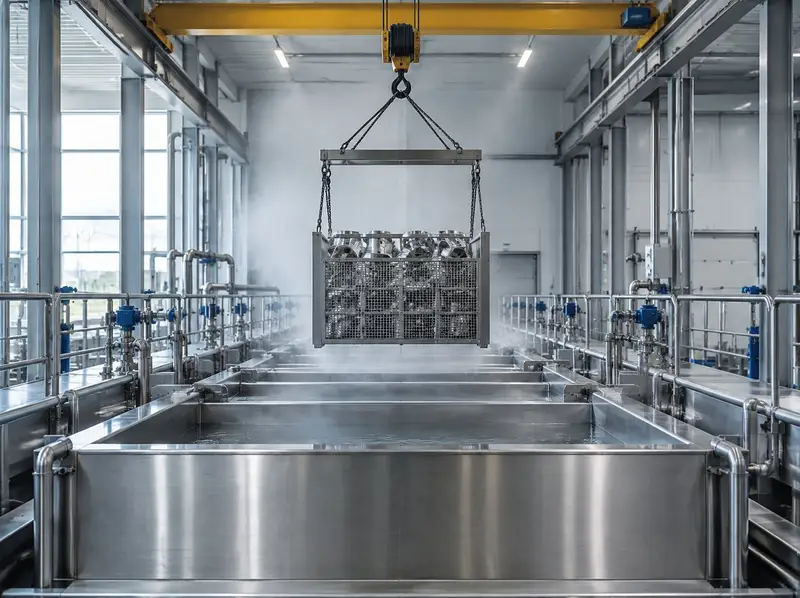
Pickling dissolves scale in an 8-tank, steam-heated line with overhead crane. Then lapping for very flat surfaces, laser marking for permanent part and lot numbers, and spray painting.
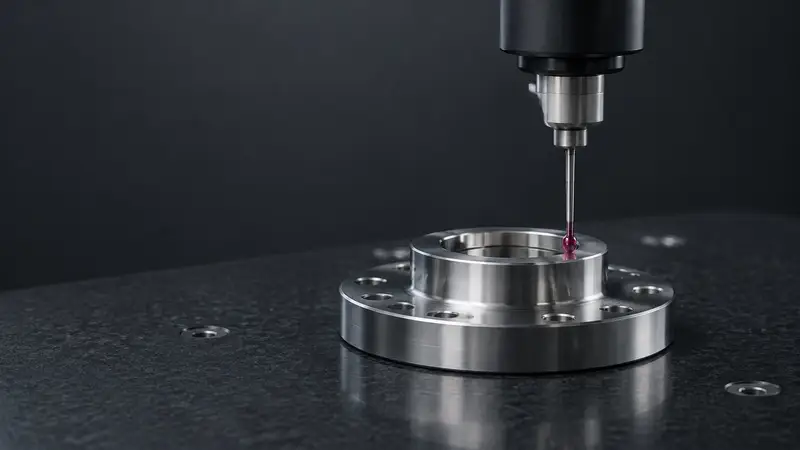
Every part can be traced back to its material, its machine and its operator.
Capability varies by part geometry, material and size. Confirm each requirement against your quotation.
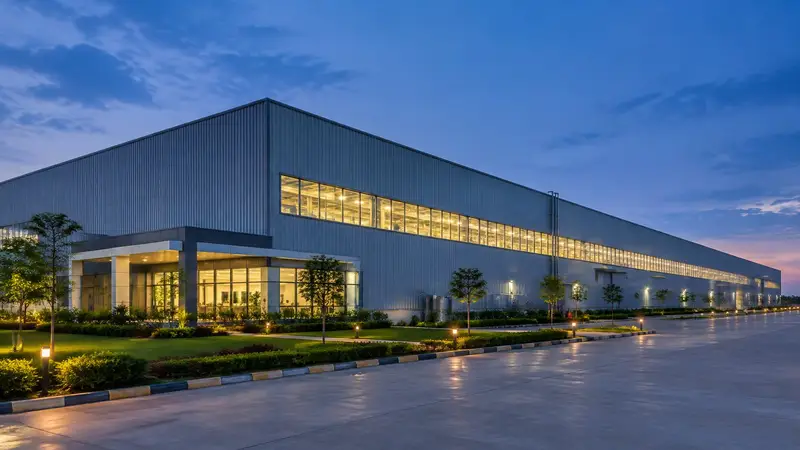
Two plants in Hyderabad, each equipped for different stages of production.
Industries we make parts for: Aerospace · OEMs
With material and quantity.
Within 24 hours of your drawing.
First parts fully measured and reported before production.
Traceable lots with material certificates and GST invoice.
A clear quote within 24 hours of your drawing.